
15 Degree Engraving 0.005 Tip Width - Amana 45611-K
15 Degree Engraving 0.005 Tip Width - Amana 45611-K
Purchase the bit: Amazon
Feeds and Speeds
Feeds and Speeds
- Walnut face grain: 12,000 RPM / Feed: 15 IPM / Plunge: 15 IPM
- Cherry face grain: 14,000 RPM / Feed: 20 IPM / Plunge: 15 IPM
- Hardwood end grain (or less details): 18,000 RPM / Feed: 54 IPM / Plunge: 18 IPM
- Stepover: 0.0024 in
Parameters for 0.100" depth inlay
Parameters for 0.100" depth inlay
inlay_depth: 0.100”inlay_fit_adjustment: 0.060” (up to 0.070”)plug_surface_gap: 0.050”plug_base_thickness: 0.250
Parameters for 0.240" depth inlay
Parameters for 0.240" depth inlay
inlay_depth: 0.240”inlay_fit_adjustment: 0.090”plug_surface_gap: 0.070”plug_base_thickness: 0.240”plug_fuzzy_cleanup: 0.008”
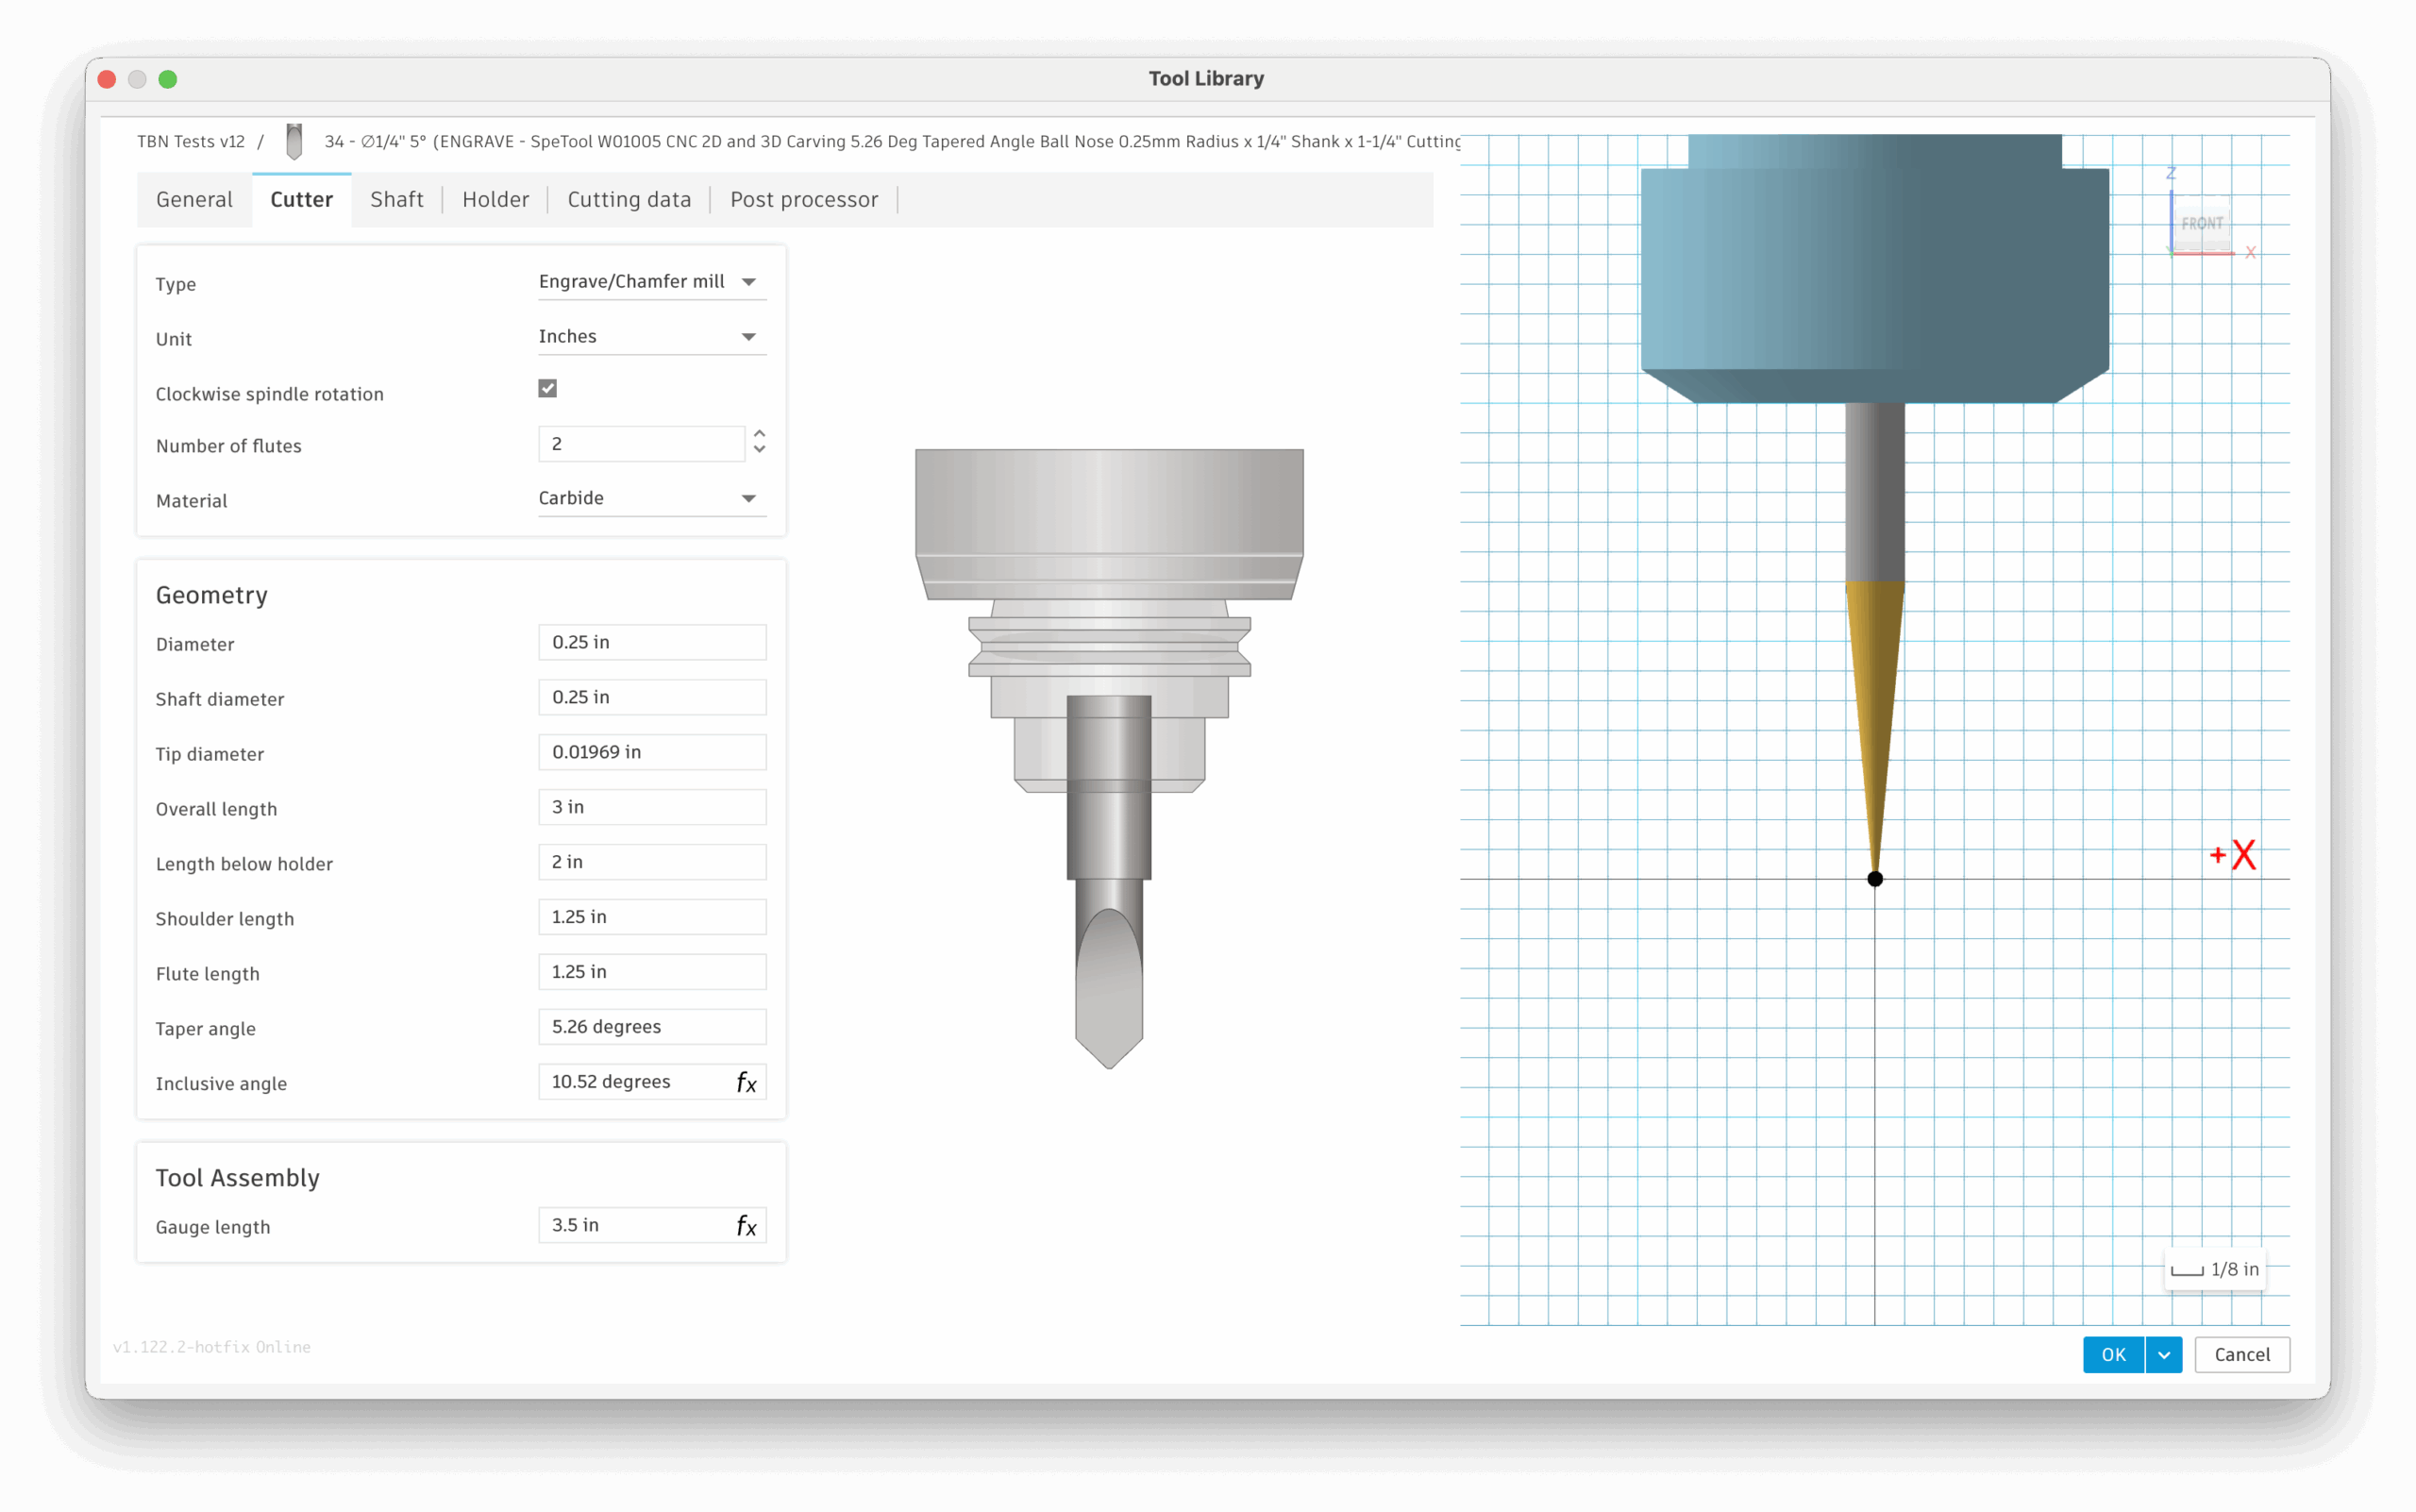
SpeTool W01005 5.26 Deg Tapered Angle Ball Nose 0.25mm Radius
SpeTool W01005 5.26 Deg Tapered Angle Ball Nose 0.25mm Radius
Feeds and Speeds
Feeds and Speeds
- End Grain: 18,000 RPM / Feed; 25.2 IPM / Plunge: 12 IPM
- Stepover: 0.0024 in
Parameters for 0.240" depth inlay
Parameters for 0.240" depth inlay
inlay_depth: 0.240”inlay_fit_adjustment: 0.000” to 0.005”
Bit Tool Setup
Bit Tool Setup
30° 2 Flute V-Groove Bit - Bits&Bits (425-VG30)
30° 2 Flute V-Groove Bit - Bits&Bits (425-VG30)
- Bit link
- 30 degree v-bit, 0” tip width (you must set a small tip width in the tool setup!)
Feeds and Speeds
Feeds and Speeds
- Facegrain: 16,000 RPM / Feed: 40 IPM / Plunge: TBD
- Feed optimization: 5 degree change, 10 IPM
Parameters for 0.240" depth inlay
Parameters for 0.240" depth inlay
inlay_fit_adjustment: 0.030”
Need help? Join Corbin’s Facebook group CNC Woodworking or email corbin@corbinsworkshop.com